Why the Cheapest Terminal Blank Can Cost More: Forging vs. Casting vs. Machining
Summary
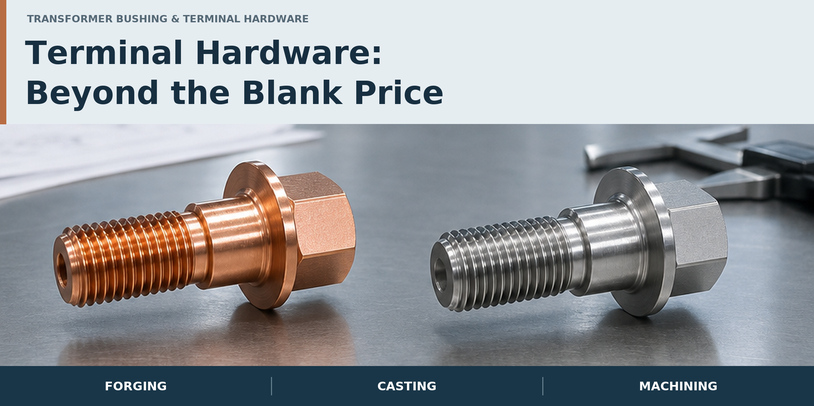
A transformer terminal can be forged, cast, or machined from billet and still pass inspection. That doesn’t mean the three parts will perform the same. Each route leaves a different grain structure and different fatigue performance, and each blank needs a different amount of machining before it can seal, thread, and carry current. Volume gives you a starting point. If the terminal sees cyclic loading, impact, or fault-current forces, its properties should pick the route first. Learn how forging, casting, and machining stack up for bushing and terminal hardware, why blank price can mislead, and what to put on the drawing to get quotes you can compare.
KEY TAKEAWAYS
ARTICLE
Three suppliers quote the same transformer terminal hardware drawing. One proposes forging. Another casting. The third wants to machine it from billet.
All three can meet the print. So why are the prices so different? And are you even comparing the same finished part?
For transformer OEM engineers and sourcing teams, choosing between forging, casting, and machining isn’t just a question of unit price. The manufacturing route affects grain structure, fatigue performance, material utilization, and the machining needed to finish critical surfaces.
A bushing terminal has to carry current, seal against oil, hold a torqued connection, and survive decades of service. The right process needs to deliver all of that, not just the lowest quote.
When manufacturing method affects performance, that choice belongs on the drawing. Left open, the lowest quote makes it.
What Forging Does to the Grain
Forging pushes metal into a die, and the grain structure deforms as the material flows. On a well-designed forging, the grain follows the part’s contours, curving around fillets and wrapping holes instead of ending at them. The part meets its load with a more favorable grain orientation.
Casting starts as liquid, so it doesn’t develop the mechanically directed grain flow of a forging. Machining from billet retains the bar stock’s existing grain orientation and cuts through it as material is removed. A machined fillet can intersect grain that originally ran lengthwise through the stock.
For static loads, differences may be modest when each part is properly designed and sized. They become more important under fatigue, impact, and stress concentrations.
That makes the deciding question how the part is loaded, not just how much load it carries.
Forging vs. Casting vs. Machining for Terminal Hardware
| Forging | Casting | Machining from Billet | |
|---|---|---|---|
| Grain structure | Can follow part geometry and load path | Determined by solidification; no forged grain flow | Retains starting stock orientation |
| Fatigue performance | Often favorable with properly designed grain flow | Depends on alloy, soundness, and defects | Depends on material and grain orientation |
| Geometric freedom | Limited by die design and forming requirements | Excellent | Excellent, subject to tool access |
| Tooling cost | High | Moderate to high | None beyond fixturing |
| Material utilization | Good | Excellent | Poor |
| Typical volume | ~1,000 a year and up | ~500 a year and up | 1 to a few hundred a year |
Typical volume ~1,000 a year and up ~500 a year and up 1 to a few hundred a year. These are general manufacturing comparisons. Actual properties, process capabilities, and economics depend on alloy, component geometry, heat treatment, quality requirements, and supplier.
Why Blank Price Is the Wrong Comparison
No matter which route makes the blank, nobody ships a finished terminal straight out of the forge, the foundry, or the bar stock. Sealing faces, threads, and contact surfaces still have to be machined. When you line up three blank prices, you’re comparing three numbers that leave out the finishing.
What matters is what each blank hands the machinist.
A forging usually shows up with a modest, consistent layer of extra material over solid metal. A casting can look perfectly sound on the outside and still hide porosity just under the surface. Often nobody finds it until the cutter opens it up, and by then you’ve already paid for the machining.
Where that porosity breaks through matters. On a sealing face, it can become a leak path. In a thread, it leaves less solid metal to grip than the drawing assumes.
The consistency of that extra material is the other cost a blank quote won’t show you. When it’s well controlled, the machinist can take a light, predictable cut on every part. When it varies, every part gets a heavier cut sized for the worst blank in the lot.
You pay for that in cycle time, in material removed, and sometimes in scrap.
Where the Volume Breakpoints Fall
Below about 200 pieces a year, machining from billet often wins. There’s no dedicated forming tooling to amortize, and a design change doesn’t scrap a die.
From about 200 to 1,000 pieces, casting tooling starts to pay back. Above about 1,000, forging and casting tooling become easier to amortize, and the choice goes back to how the part is loaded.
These are general starting points. Actual break-even volumes depend on part geometry, alloy, tooling investment, finishing costs, and annual demand.
A terminal torqued once at installation and subject primarily to static loading may be a reasonable casting candidate. A lug carrying a rated mechanical load, a connector repeatedly torqued during maintenance, or a component exposed to fault-current forces presents a different case.
That’s a properties decision, and production volume doesn’t override it.
Choose the Material and the Route Together
The three routes don’t offer the same material options. A drawing written without that in mind can leave the manufacturing route determined by alloy availability rather than engineering requirements.
Copper is well suited to forging and machining in many grades, while casting suitability depends on the alloy and process.
Cast stainless grades also differ from their wrought counterparts. CF8M is the cast counterpart of wrought 316 stainless steel, but it has its own material specification and composition limits. It isn’t simply wrought 316 poured into a mold.
When a drawing calls for wrought 316 and a supplier quotes CF8M, the proposal involves a material substitution, not just a different production process.
That substitution needs engineering review to confirm the mechanical properties, corrosion resistance, and applicable qualification requirements.
What to Put on a Bushing or Terminal Hardware Drawing
Two of these deserve a closer look.
Grain flow serves as a practical indicator of the intended forging structure. Fatigue performance is expensive to verify through testing of production parts, so a grain flow requirement with a sectioning and etching method helps establish whether the forging has the intended orientation.
Ultrasonic testing is more challenging on some castings. Coarse or complex as-cast grain structures can interfere with the signal. That’s one reason forged components may be preferred when demanding subsurface inspection requirements apply.
Choose the Route Before the Quotes Do
A drawing that specifies geometry, material, and finish but leaves the manufacturing process open invites all three routes to quote.
The prices often come back very different, for parts with different fatigue characteristics and finishing requirements.
MES forges, casts, and machines bushing and terminal hardware across eight countries. Heat-lot traceability is captured at the mill, not reconstructed on receipt. Every drawing gets an engineering review before a tool is cut.
Send Us Your Terminal Hardware Drawing
Share your drawing, annual volume, and how the part is loaded in service. An MES engineer can evaluate which manufacturing route best meets the component’s requirements and production economics.
Frequently Asked Questions
Why are terminal lugs forged rather than cast?
For most direct-to-chip applications, 0.025 mm across the die contact footprint is a good working specification. A controlled CNC operation can usually hold it in a single setup. Below about 0.015 mm, a secondary operation such as grinding or dedicated fly cutting is often required, significantly increasing manufacturing cost. The flatness tolerance should reflect what the thermal model needs.
Is a forged part always stronger than a cast one?
No. Static strength depends on material, geometry, processing, and quality. A properly designed casting or machined component may meet the same static load requirements as a forging. Forging can offer advantages under fatigue, impact, and stress concentrations because of its grain flow and material consolidation.
At what volume does forging become cheaper than machining?
Around 1,000 pieces a year is a useful starting point, although the breakpoint changes with part complexity, alloy, tooling investment, and finishing requirements. Below about 200 pieces, machining from billet is often economical because there’s no dedicated forming die to amortize. At higher volumes, compare forging and casting based on finished-part cost and service requirements.
What does casting porosity mean for machined terminal hardware?
Subsurface porosity may remain hidden until machining exposes it. If it intersects a sealing face, it can create a potential leak path. In a threaded region, it can reduce the amount of sound material available for engagement. Because machining costs may already have been incurred when the defect is discovered, porosity can affect both finished-part quality and production economics.
Can CF8M replace 316 stainless steel in terminal hardware?
Not automatically. CF8M is the cast counterpart of wrought 316 stainless steel, but it has its own material specification and composition limits. Substituting CF8M for wrought 316 requires engineering review to verify that the component meets its mechanical, corrosion-resistance, and qualification requirements.
Should a terminal hardware drawing specify the manufacturing route?
The tolerance usually stays the same while the span grows. Holding 0.025 mm across 30 mm is 1 part in 1,200, and across 70 mm it’s 1 part in 2,800. Residual stress relaxation, heat from the cut, and fixture distortion all act over more than twice the distance.