Why a Thin Skived Fin Can Cost Up to 3× More: Aspect Ratio Limits for Data Center Cold Plates
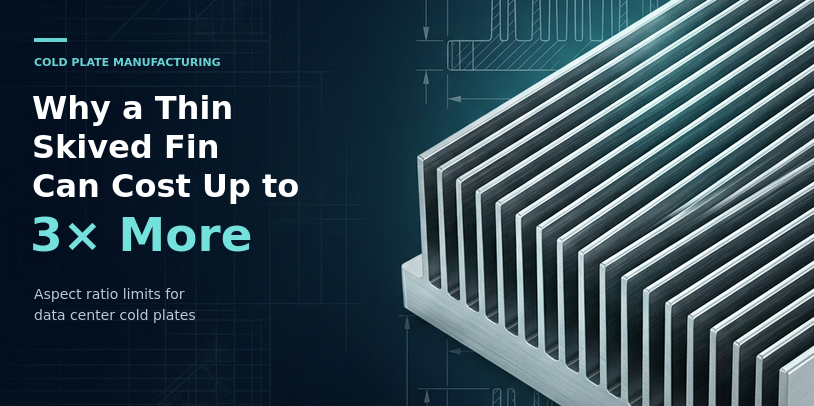
A fin drawing that looks reasonable can come back quoted at 2 to 3 times the expected price. The reason is usually aspect ratio. Here’s how to evaluate skived fin designs in light of the practical limits of copper and aluminum, plus what to know before requesting a supplier quote.
Skiving Limits for Cold Plates: Is Your Fin Design Ready for Production?
Summary
Skived fins are one of the most common ways to build the heat transfer surface inside liquid-cooled cold plates for high-density AI data centers, but every skived fin design has a practical manufacturing limit. The practical limit depends on fin aspect ratio (height divided by thickness), material properties, and blade condition. Inside the comfortable range, yield is high and pricing is predictable. Near the limit, scrap rises and supplier quotes can vary by 2 to 3 times. Learn why copper can be skived into thinner, taller fins than aluminum, and what to check before sending a fin drawing out for supplier quotes.
KEY TAKEAWAYS
ARTICLE
Many enterprise data center racks operate well below 10 kW. A liquid-cooled AI rack such as NVIDIA’s GB200 NVL72, by comparison, is rated at roughly 120 kW. At that density, cold plates carry much of the heat load, and skived fins provide the heat-transfer surface needed to help keep critical components cool.
MES sees a recurring challenge in the fin drawings it reviews. A customer specifies copper fins just 0.25 mm thick and 9 mm tall, only to receive manufacturing quotes 2 or 3 times higher than expected.
The problem may be the geometry itself. At those dimensions, the fins have an aspect ratio of 36:1, beyond the range where copper skiving typically delivers consistent production yields. Root cracking, fin buckling, and tooling wear can increase scrap, and suppliers must account for those losses in their pricing.
Knowing where a design falls relative to practical skiving limits helps engineers and sourcing teams decide whether to negotiate the quote or revisit the fin specifications before production begins.
Start with the Fin Aspect Ratio
Fin height and thickness tell only part of the manufacturing story. The more important consideration is the relationship between them.
Aspect ratio = Fin height ÷ Fin thickness
Consider two copper fin designs:
| Fin Height | Fin Thickness | Aspect Ratio |
|---|---|---|
| 8 mm | 0.3 mm | About 27:1 |
| 13 mm | 0.5 mm | 26:1 |
The second fin is considerably taller, but its aspect ratio is almost identical. From a geometric standpoint, both designs present a similar skiving challenge.
As aspect ratio increases, it generally becomes more difficult to form fins without defects and maintain consistent production yields.
What Happens During Skiving?
Unlike conventional machining, which removes material, skiving uses a blade to lift and bend a thin layer of metal into a fin that remains attached to the base. Each fin bends roughly 90 degrees at its root, putting considerable strain on the material.
That localized bending introduces 3 manufacturing risks:
- Root cracking: Thinner fins experience greater strain where they join the base. Partial cracks can reduce the heat-transfer path without being obvious during routine visual inspection.
- Fin buckling: Tall, slender fins can deform during forming or cleaning, narrowing coolant channels and affecting flow distribution.
- Blade deflection and wear: Cutting forces can change fin thickness, while blade wear can reduce dimensional consistency and yield throughout a production run.
These risks help explain why a supplier may successfully produce a few samples but struggle to manufacture the same design economically at scale.
Skived Fin Limits: How Close Is Your Design to the Maximum?
The same fin geometry that works in copper may be difficult or uneconomical to produce in aluminum. That’s because each material responds differently to the bending and strain involved in skiving.
The table below compares typical production limits for 3 commonly used materials in liquid-cooled cold plates.
Skived Fin Thickness, Height, and Aspect Ratio by Material
| Design Parameter | C11000 Copper | 6063-T5 Aluminum | 1100 Aluminum |
|---|---|---|---|
| Minimum fin thickness | 0.15–0.20 mm | 0.30–0.40 mm | 0.25–0.35 mm |
| Comfortable aspect ratio | 25–30:1 | 15–18:1 | 18–22:1 |
| Maximum aspect ratio | 35–40:1 | 20–25:1 | 25–30:1 |
| Maximum fin height | 20–25 mm | 15–18 mm | 15–20 mm |
| Minimum fin pitch | 0.30–0.40 mm | 0.60–0.80 mm | 0.50–0.70 mm |
These are typical production ranges, not guaranteed limits. Equipment, blade design, material condition, and process controls can affect what’s achievable.
Comfortable vs. Maximum: There's a Cost Difference
Comfortable production range: Fin geometry that generally supports consistent manufacturing yields and more predictable pricing.
Maximum practical range: Geometry that may be achievable but carries greater risk of cracking, dimensional variation, and scrap, especially at production volume.
“Most of the fin drawings we review are designed close to the maximum column,” says Brad Layne, Engineering Manager at MES. “We’d rather have that conversation before tooling is built, because moving a design back into the comfortable range usually costs much less than paying for scrap over the life of the program.”
Why Copper Can Handle Taller, Thinner Fins
Copper generally supports higher skived fin aspect ratios than aluminum because it can tolerate greater localized deformation.
C11000 copper has high elongation and work hardens gradually, allowing the fin root to withstand a tight bend. By comparison, artificially aged 6063-T5 aluminum has lower ductility. The more ductile 1100 aluminum falls between the two in practical skiving capability.
The design implication: A 30:1 aspect ratio may be within the comfortable production range for C11000 copper but beyond the typical maximum for 6063-T5 aluminum. Material selection needs to account for skiving feasibility alongside thermal performance and cost.
Skived Fin Limits: How Close Is Your Design to the Maximum?
A supplier may be able to produce a copper skived fin at 35:1, but that doesn’t mean the process will deliver consistent yields across a production run.
As aspect ratio increases, root cracking becomes more frequent, blade condition has a greater influence, and scrap rates can rise. Those costs get built into the quote.
Copper Skived Fin Aspect Ratio: Yield and Pricing
| Aspect Ratio | Production Behavior | Pricing Impact |
|---|---|---|
| Up to about 25:1 | High yield, stable production | Predictable |
| 25–30:1 | Good yield, more frequent blade changes | Modest premium |
| 30–35:1 | Intermittent root cracking, declining yield | Depends on expected scrap |
| 35–40:1 | Significant yield variation, greater sensitivity to blade condition | Quotes may vary widely |
| Above about 40:1 | Samples may be possible, but production isn’t stable | Generally unsuitable for production quoting |
Illustrative ranges for C11000 copper. Actual results depend on equipment, material condition, and tooling.
At an aspect ratio around 35:1, quotes can differ by a factor of 2 or 3 because suppliers anticipate different scrap rates.
A higher quote isn’t necessarily evidence of an overpriced supplier. It may reflect a more realistic estimate of manufacturing risk.
Before negotiating price, ask what production yield the supplier has assumed and whether a small change in fin geometry could reduce scrap.
3 Checks Before Requesting a Skived Fin Quote
A few straightforward checks can identify manufacturing concerns before tooling is ordered.
1. Check the Aspect Ratio
Divide fin height by thickness and compare the result with the comfortable production range for the selected material.
A geometry near the maximum deserves closer review, particularly for higher-volume programs.
2. Calculate the Open Channel Width
Fin pitch includes both the fin and the space next to it.
Channel width = Fin pitch − Fin thickness
For example, a 0.40 mm pitch with a 0.25 mm fin leaves a 0.15 mm channel.
Gaps below about 0.15 mm can be difficult to clean and inspect. Channel clearance must also accommodate the cold plate’s coolant flow requirements.
3. Verify Remaining Base Thickness
Confirm that the material remaining beneath the fins after skiving can meet the required flatness and structural specifications.
If any of these checks raises concerns, discuss the geometry with the manufacturer before requesting a firm production quote.
When Should You Change the Fin Design?
A fin design approaching the skiving limits doesn’t necessarily require a complete redesign. Small adjustments may improve production yield, although each has implications for thermal performance.
| Design Adjustment | Manufacturing Benefit | Engineering Consideration |
|---|---|---|
| Increase fin thickness and pitch | Reduces aspect ratio and root strain | May reduce heat-transfer surface area |
| Reduce fin height | Improves forming stability | May require changes to coolant velocity, subject to pressure-drop limits |
| Consider brazed fin stock | Can support aspect ratios around 50:1 | Adds a joint at every fin root |
None of these changes should be made based on manufacturing cost alone. The revised geometry still needs to meet the cold plate’s thermal and hydraulic requirements.
The goal is to find a design that delivers the necessary cooling performance at an acceptable production cost.
What to Include on a Skived Fin Drawing
Even a manufacturable design can generate inconsistent quotes if suppliers have to make assumptions about dimensions or inspection requirements.
Before releasing your RFQ, check that the drawing specifies:
These details give suppliers a consistent basis for assessing manufacturing feasibility, inspection requirements, and production costs.
Design for Production, Not Just the First Sample
A cold plate fin design that performs well in a prototype may be expensive to manufacture consistently at production volume.
Near the limits of skiving, even small changes in thickness, height, or pitch can affect yield and cost. Identifying those opportunities early gives engineers more flexibility and helps sourcing teams avoid unexpected expenses.
MES supplies skived copper and aluminum cold plates through its manufacturing network across eight countries. Our engineering team reviews fin geometry, material selection, and practical production limits before tooling begins, helping customers evaluate manufacturability before committing to a design.
Send Us Your Fin Specification
Have a cold plate fin design ready for review? Share your fin thickness, height, pitch, material, and anticipated production volume. An MES engineer can help evaluate the geometry and discuss manufacturing options.
Talk to an MES engineer about your fin geometry and pricing.
Frequently Asked Questions About Skived Fin Cold Plates
How thin can a skived fin be?
In C11000 copper, practical minimum thickness is about 0.15 to 0.20 mm, while 0.25 to 0.40 mm can offer more comfortable production yields, depending on fin height and pitch. For 6063-T5 aluminum, the typical minimum is about 0.30 to 0.40 mm.
What is the maximum aspect ratio for a skived fin?
C11000 copper typically supports maximum aspect ratios of about 35:1 to 40:1, compared with 20:1 to 25:1 for 6063-T5 aluminum. Comfortable production ranges are lower, generally around 25:1 to 30:1 for copper. Actual limits depend on equipment, blade design, and material condition.
Why does copper skive better than aluminum?
Skiving bends each fin sharply at its root, making ductility under high localized strain especially important. C11000 copper has greater elongation and work hardens gradually, allowing more aggressive fin geometries than artificially aged 6063-T5 aluminum.
What happens if a fin specification exceeds practical manufacturing limits?
Production may still be possible, but yield and pricing become less predictable. Root cracking, buckling, and tooling wear can increase scrap rates. Different assumptions about production losses can lead to quotes that vary by 2 or 3 times.
What should a skived fin drawing specify?
Include fin thickness with a tolerance and measurement location, pitch tolerance, fin height, remaining base thickness, material and temper, and root-cracking acceptance criteria. Define the inspection method so suppliers evaluate the same requirements.
Can skived fins have variable density across a cold plate?
Conventional skiving produces straight, parallel fins at a consistent pitch within a single fin field. Designs requiring different fin densities across a plate may need machined channels or separately manufactured brazed fin sections.